



How to Choose an Industrial LED Supplier for Factory Lighting Projects
November 6, 2026
For procurement and facility managers overseeing manufacturing plants, warehouses and industrial sites, selecting factory lights LED is far more than a component purchasing decision — it is a long-term investment in production safety, operational efficiency and energy cost control.
Factory environments present harsh operating conditions: heavy dust, high humidity, wide temperature swings, continuous 24/7 operation and even mechanical vibration.
Standard commercial lighting fixtures cannot withstand these conditions, and partnering with an inexperienced industrial LED supplier leads to premature failure, frequent maintenance, elevated energy consumption and even production downtime caused by lighting outages.
Too many procurement teams select suppliers based on upfront price alone, ignoring industrial-grade reliability and total cost of ownership.
Why Factory Lighting Requires Industrial-Grade Suppliers
Ordinary commercial LED fixtures work well in offices and retail spaces, but they are not engineered for the realities of industrial environments. The consequences of using non-industrial grade products in factory settings go far beyond shorter service life.
For these reasons, factory LED procurement must prioritize industrial-grade design and supplier capability over initial unit cost.
Core Evaluation Criteria for Industrial LED Suppliers
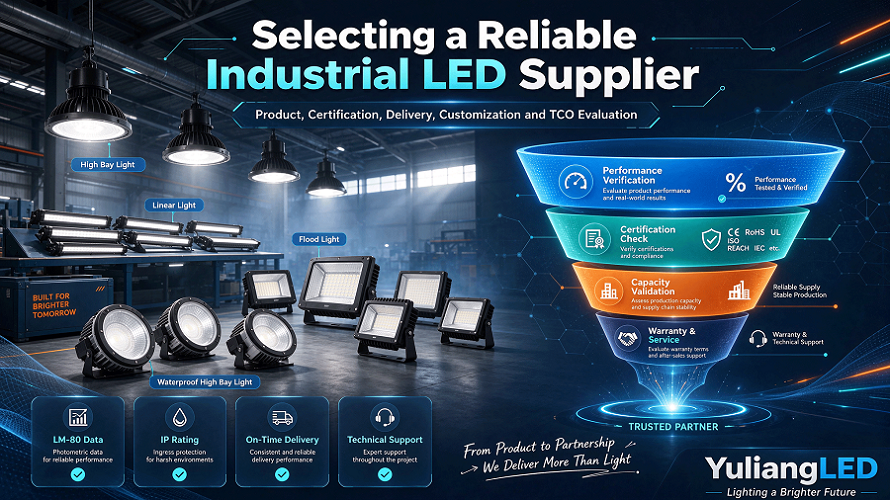
Use this six-dimension framework to systematically compare suppliers and identify partners that can truly support industrial-scale installations.
1. Product Performance: Engineered for Industrial Conditions
Performance claims are easy to make — verified specifications are what matter. A credible industrial LED supplier provides full, test-backed performance data for every fixture model.
2. Compliance & Certifications: Verifiable, Not Just Printed
Industrial lighting is subject to strict safety, electrical and environmental regulations. Certifications protect you from compliance risk, import issues and liability in case of electrical incidents.
3. Production Capability & Delivery Reliability
Large factory retrofit projects and ongoing rollout programs require consistent output and predictable lead times. A supplier that performs well on a small sample order may struggle to maintain quality and schedule at volume.
4. Customization & Technical Support
Every factory has different ceiling heights, aisle layouts, ambient conditions and illumination targets. A supplier that only offers catalog products cannot deliver an optimized solution.
A professional industrial LED supplier acts as a solution partner, not just a product vendor. They help you select the right fixture type, quantity and layout for your specific site, not push the highest-wattage or cheapest model.
5. Warranty & After-Sales Service
Industrial lighting operates for years under stress conditions, and warranty coverage directly affects your total cost of ownership.
PREVIOUS ARTICLE